Porosity & Quality
Checklist: Verifying Porosity Prevention in Supplier Quotes
Validate porosity prevention verification in supplier quotes by checking process control, supplier quality audit scope, and defect testing plans. This checklist helps

Root causes and prevention of porosity, shrinkage, and other common die casting defects.
Validate porosity prevention verification in supplier quotes by checking process control, supplier quality audit scope, and defect testing plans. This checklist helps
External labs add independent verification for die casting porosity. Select providers by matching their analytical methods to your material and defect profile. Confirm
Automated porosity monitoring uses AI and X-ray systems to detect internal defects in real time. It reduces manual inspection load and helps procurement teams verify
Importers and procurement managers should evaluate external defect prevention services by checking technical depth, audit protocols, and data integration. The right
X-ray imaging offers a visual, two-dimensional view of internal porosity, making it ideal for complex geometries and audit trails. Ultrasonic testing detects deeper
Shrinkage in aluminum die casting occurs when metal cools and solidifies, leaving internal voids. You can reduce these defects by stabilizing melt chemistry, optimizing
This checklist provides a framework for procurement managers to evaluate supplier quotes for porosity prevention. It covers process controls, inspection methods, and
Shrinkage in zinc parts stems from poor feeding, high temperatures, or slow cooling. This guide lists specific process adjustments to eliminate the defect, including
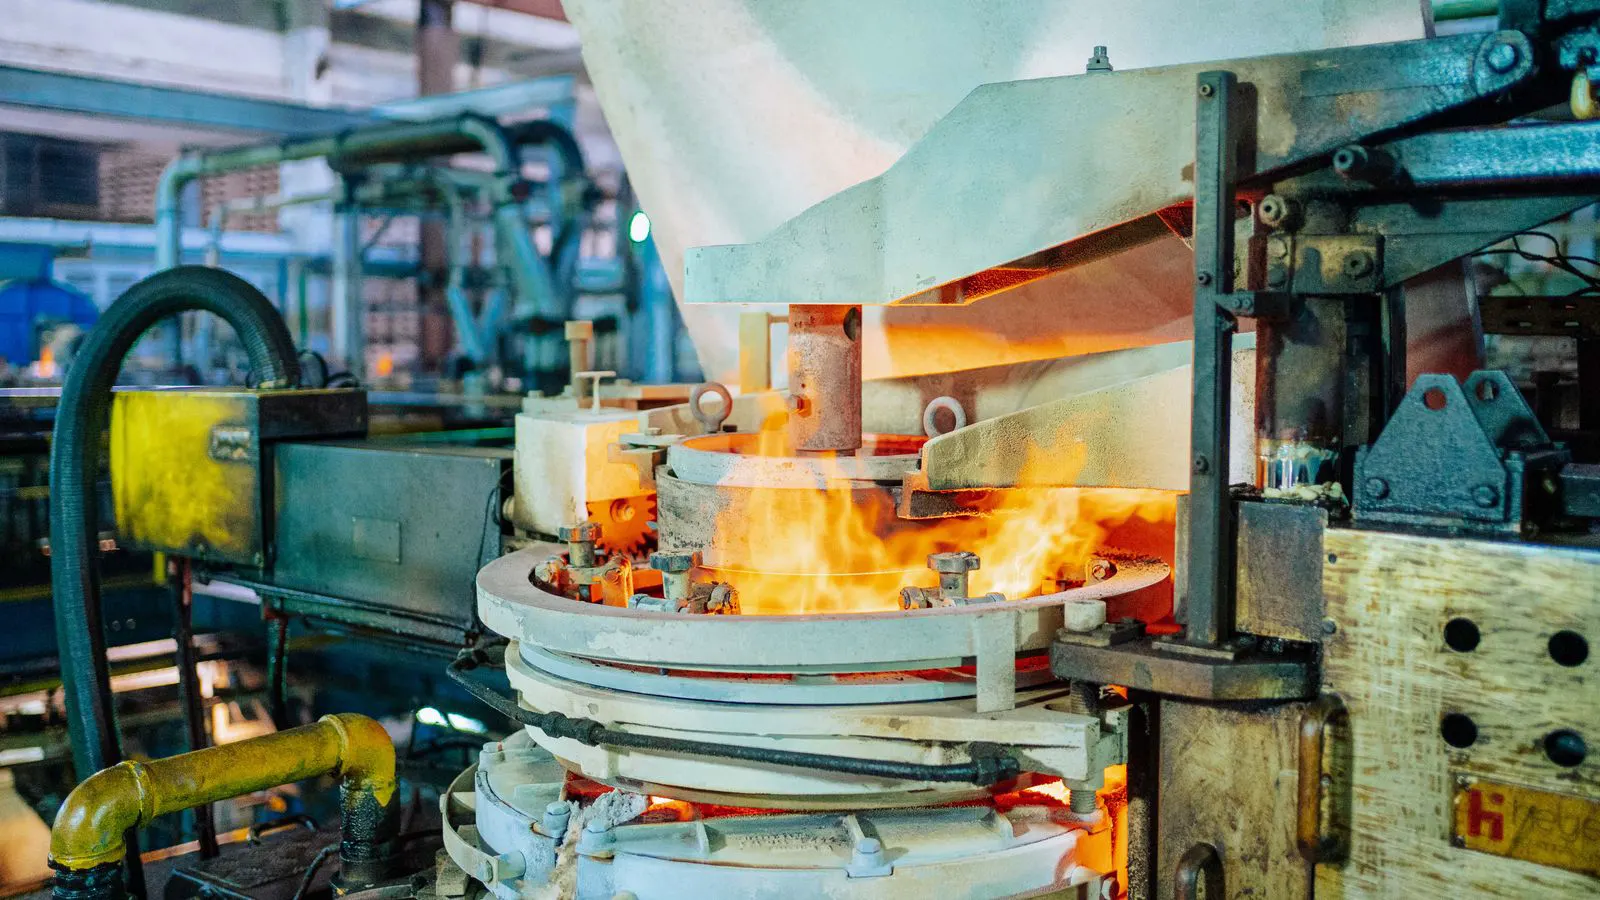
Gas porosity forms from trapped air or hydrogen, while shrinkage porosity forms as the metal solidifies and cools. Gas pores are often surface-level and irregular
Gas porosity forms when dissolved gases escape the melt as bubbles trapped in the die. Melt chemistry, temperature, and flow control determine which defects appear. This
X-ray inspection provides internal defect visibility for die castings without destroying the part. Buyers must evaluate resolution, throughput, and data integration to
High-speed aluminum die casting creates gas pockets when melt temperature is too low or injection pressure is insufficient. This guide outlines how to adjust machine