Aluminum Die Casting Porosity: Causes and Fixes
Aluminum die casting porosity is caused by trapped gas or poor metal flow. This guide lists common symptoms, likely causes, and fixes to improve quality control and reduce casting defects.
- Porosity is a common issue in aluminum die casting that weakens castings.
- Trapped gas and improper melt temperature are primary causes of casting defects.
- Regular quality control checks help detect internal voids before production.
- Adjusting pressure, temperature, and mold design reduces the risk of porosity.
- Proper maintenance of the die casting machine supports consistent part quality.
What Is Die Casting Porosity?
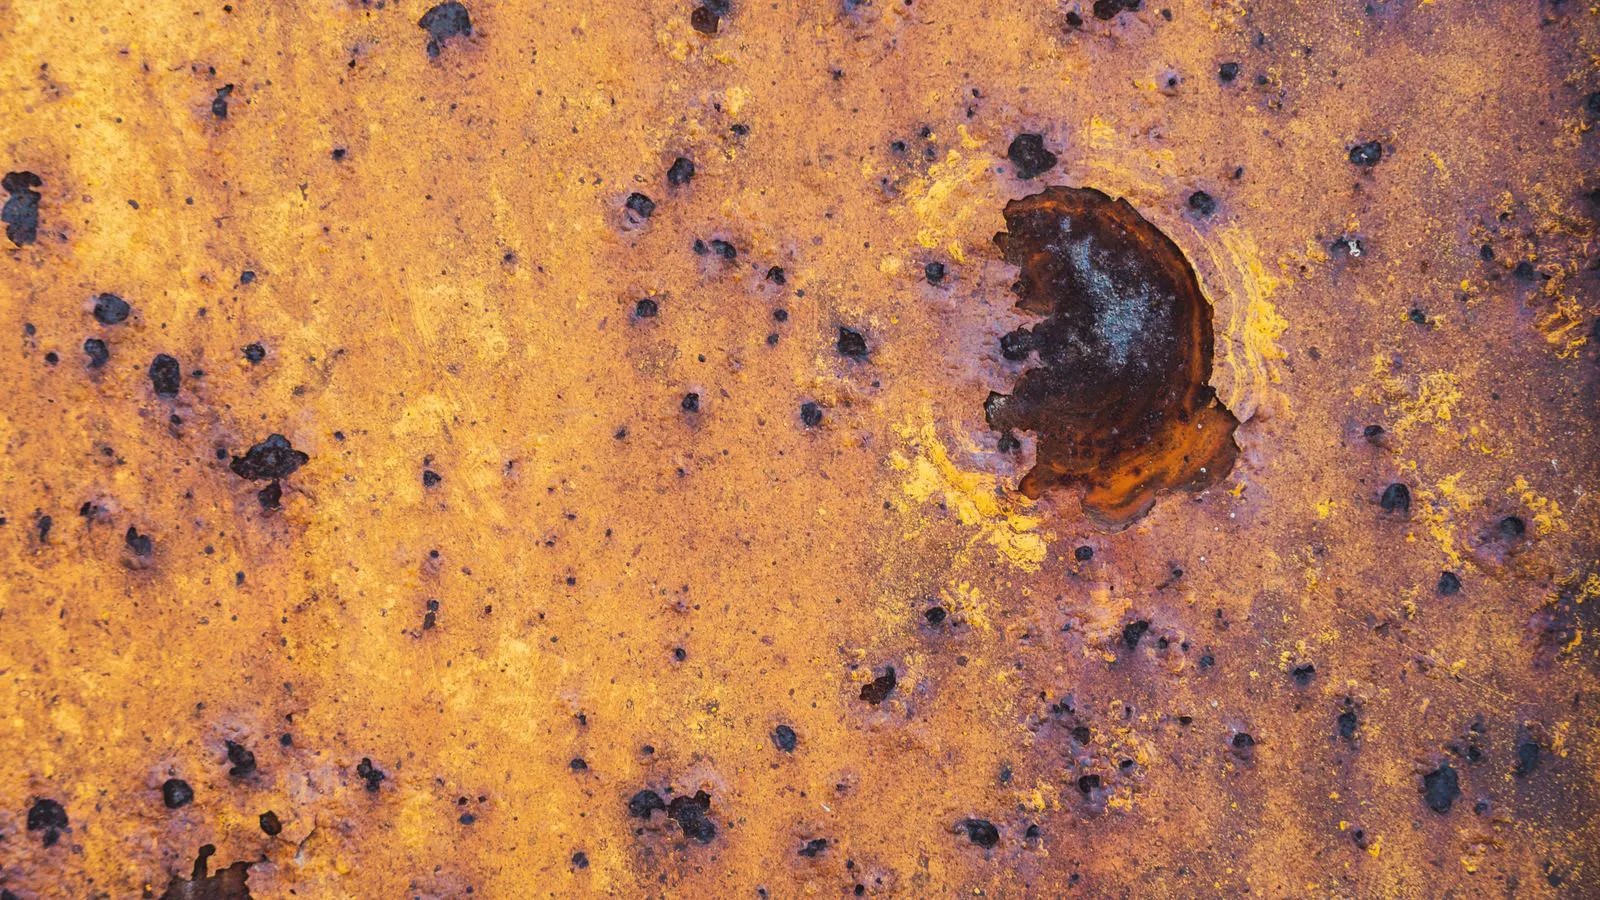
Die casting porosity refers to voids or gas pockets trapped inside or on the surface of an aluminum casting. These defects form when gas does not escape the mold during the solidification process. Even small amounts of porosity can compromise strength, appearance, or sealing performance.
Porosity can appear as internal voids or external pits. Internal voids are harder to detect and require destructive testing or radiography. Surface porosity may show as small holes or dimples. Both types indicate a breakdown in the casting process or material preparation.
Common Symptoms of Porosity in Aluminum Castings
Operators and inspectors often notice porosity through specific visual or mechanical signs. These symptoms help identify whether a defect is surface-level or internal.
- Surface pits or small holes
- Dimpled or rough casting surfaces
- Weight variation between parts
- Failed pressure tests
- Cracks forming around voids
- Visible voids during sectioning
Internal porosity may not be visible until a part is cut or tested. Weight checks are a simple way to spot abnormal voids, as a casting with internal gas will weigh less than expected.
Likely Causes of Casting Porosity
Several factors contribute to die casting porosity. Understanding these causes allows engineers to target the root issue rather than just treating symptoms.
Gas Trapping
Air and moisture in the metal or mold can become trapped during solidification. Aluminum is reactive, and if the melt is not properly covered, gas absorption increases.
Low Melt Temperature
If the molten aluminum is too cool, it flows slowly and traps gas behind itself. This is a common cause of casting defects in high-pressure die casting.
Poor Mold Venting
Inadequate venting channels prevent gas from escaping the mold cavity. This is especially common in complex die shapes or when vents become blocked.
Inconsistent Injection Pressure
Too low pressure can leave gas pockets behind. Too high pressure can cause sanding, but insufficient pressure often leads to porosity.
Contaminated Metal
Scrap with paint, oil, or moisture can introduce gas into the melt. This is a frequent source of casting defects when recycled material is not cleaned properly.
Fixing Porosity: Troubleshooting Table
The table below lists common symptoms, likely causes, and practical fixes for die casting porosity.
| Symptom | Likely cause | What to do |
|---|---|---|
| Surface pits | Gas trapped on surface | Check melt temperature and add gas absorber |
| Internal voids | Poor venting or low pressure | Improve vent design and increase injection pressure |
| Weight variation | Inconsistent metal flow | Monitor melt temperature and injection speed |
| Dimpled surface | Trapped moisture in mold | Dry the die and check for water contamination |
| Cracks around voids | Rapid cooling or gas expansion | Adjust cooling cycle and reduce thermal stress |
| Rough surface finish | Sanding from high pressure | Lower injection pressure and improve die cooling |
Prevention Tips for Quality Control
Preventing die casting porosity is more effective than trying to fix it after the fact. A strong quality control program addresses the process, materials, and equipment.
1. Monitor Melt Temperature
Keep molten aluminum within the recommended range. Too cool traps gas, and too hot burns the die or increases oxidation. Use a reliable thermometer and log readings regularly.
2. Maintain Proper Mold Venting
Inspect vents before each shift. Clean any buildup and verify that vent paths are unobstructed. Complex molds may need additional venting to prevent gas accumulation.
3. Control Scrap and Recycle
Clean scrap thoroughly to remove paint, oil, and moisture. Use scrap that is compatible with the alloy. Consistent metal quality reduces the chance of gas formation.
4. Optimize Injection Pressure
Find the pressure range that fills the mold completely without causing sanding or excessive force. Adjust based on part geometry and alloy behavior.
5. Use Gas Absorbers
Adding gas absorber to the melt can help reduce dissolved gas. Follow the manufacturer’s recommendations for the type and amount used.
6. Perform Regular Die Maintenance
Worn dies can trap gas or cause uneven cooling. Inspect for wear, corrosion, and hot spots. Keep die surfaces clean and properly lubricated.
Testing Methods for Detecting Porosity
Quality control teams use several methods to detect porosity in aluminum castings. The choice of method depends on the part’s criticality and production volume.
- Visual inspection for surface defects
- Weighing for internal voids
- Dye penetrant testing for surface porosity
- X-ray or radiography for internal defects
- Ultrasonic testing for large components
- Pressure testing for sealing applications
For high-value parts, destructive testing or radiography may be required. For production runs, visual inspection and weight checks are practical first steps.
When to Escalate a Porosity Issue
If porosity appears after process changes, pause production and review the changes. If defects persist despite corrective actions, involve the die manufacturer or metallurgist. Persistent casting defects may indicate a deeper problem with die design or alloy suitability.
Keep records of each batch, including melt temperature, pressure, and scrap source. This data helps identify trends and supports long-term quality control.
Final Thoughts
Die casting porosity is a manageable issue when identified early and addressed with the right process controls. By monitoring temperature, maintaining die condition, and using proper quality control methods, manufacturers can significantly reduce casting defects. A systematic approach to prevention leads to stronger, more reliable aluminum castings and fewer rejected parts.
Frequently asked questions
What is the main cause of die casting porosity?
The main cause is trapped gas in the mold or metal. This can result from low melt temperature, poor venting, or contaminated scrap.
Can die casting porosity be fixed after production?
Minor surface porosity can sometimes be repaired, but internal voids usually require rework or rejection. Prevention is more effective than repair.
How do I detect internal porosity in aluminum castings?
Use weighing, X-ray radiography, or ultrasonic testing. Visual inspection only detects surface-level defects.
Does high pressure always reduce porosity?
No. Too much pressure can cause sanding or die damage. The goal is sufficient pressure to fill the mold without trapping gas.
How often should I check die venting?
Check vents before each shift and after any interruption. Complex molds may need more frequent inspection to prevent gas buildup.